Industrial & Manufacturing
Security systems for pharmaceutical & medical-device manufacturing.
Regulated facilities with controlled materials, clean production, documentation, laboratories, and secure distribution.
- ★ 4.9 ratingHundreds of client reviews
- 10,000+Systems installed & serviced
- Since 2008Family-owned
- CSLB #1094834C-7 licensed, bonded & insured
- BSIS ACO #8164Licensed alarm company
Property-specific planning
Security should support the business—not get in its way.
Regulated facilities with controlled materials, clean production, documentation, laboratories, and secure distribution. A well-designed system should help the property team strengthen chain-of-custody and access accountability around regulated operations, without getting in the way of daily operations.
We look at the whole site rather than one system at a time, so cameras, alarms, and access control work as one system.
Authentic Three Factor field work
Experience grounded in real operating environments.
Representative project photography from our Southern California portfolio.
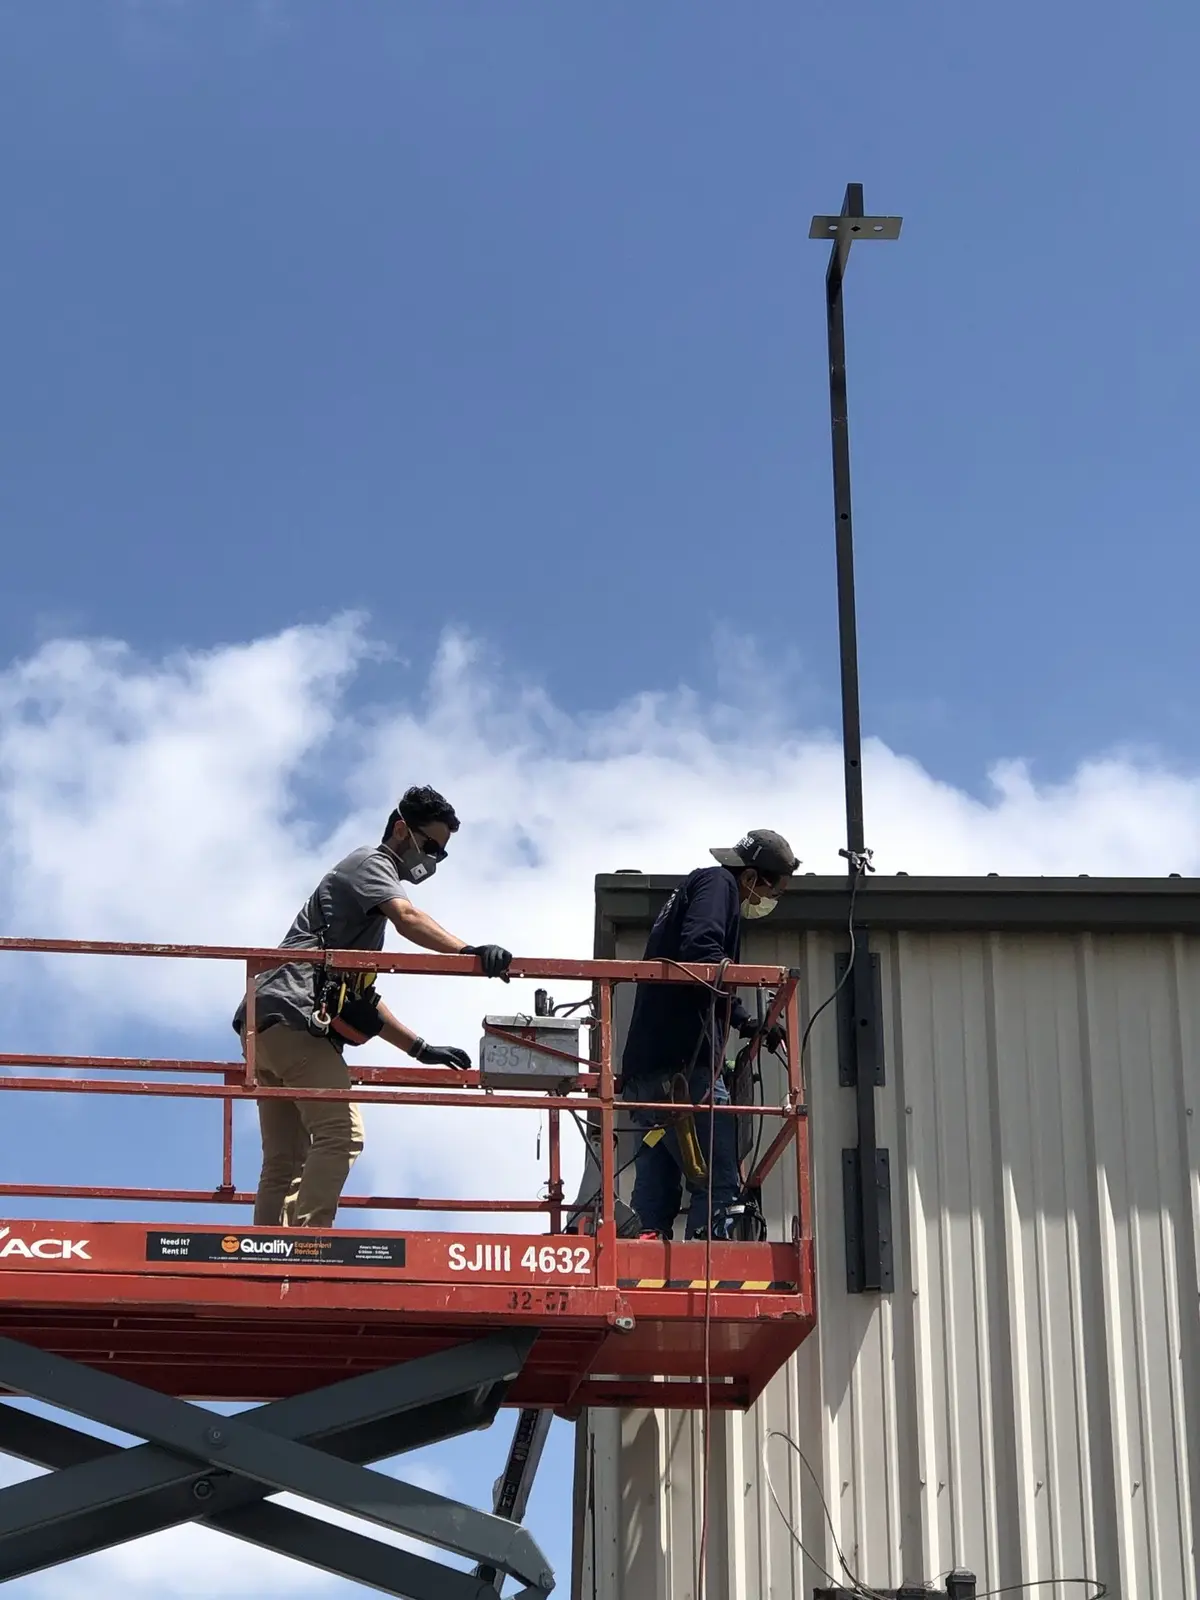 Fieldwork inCentury City
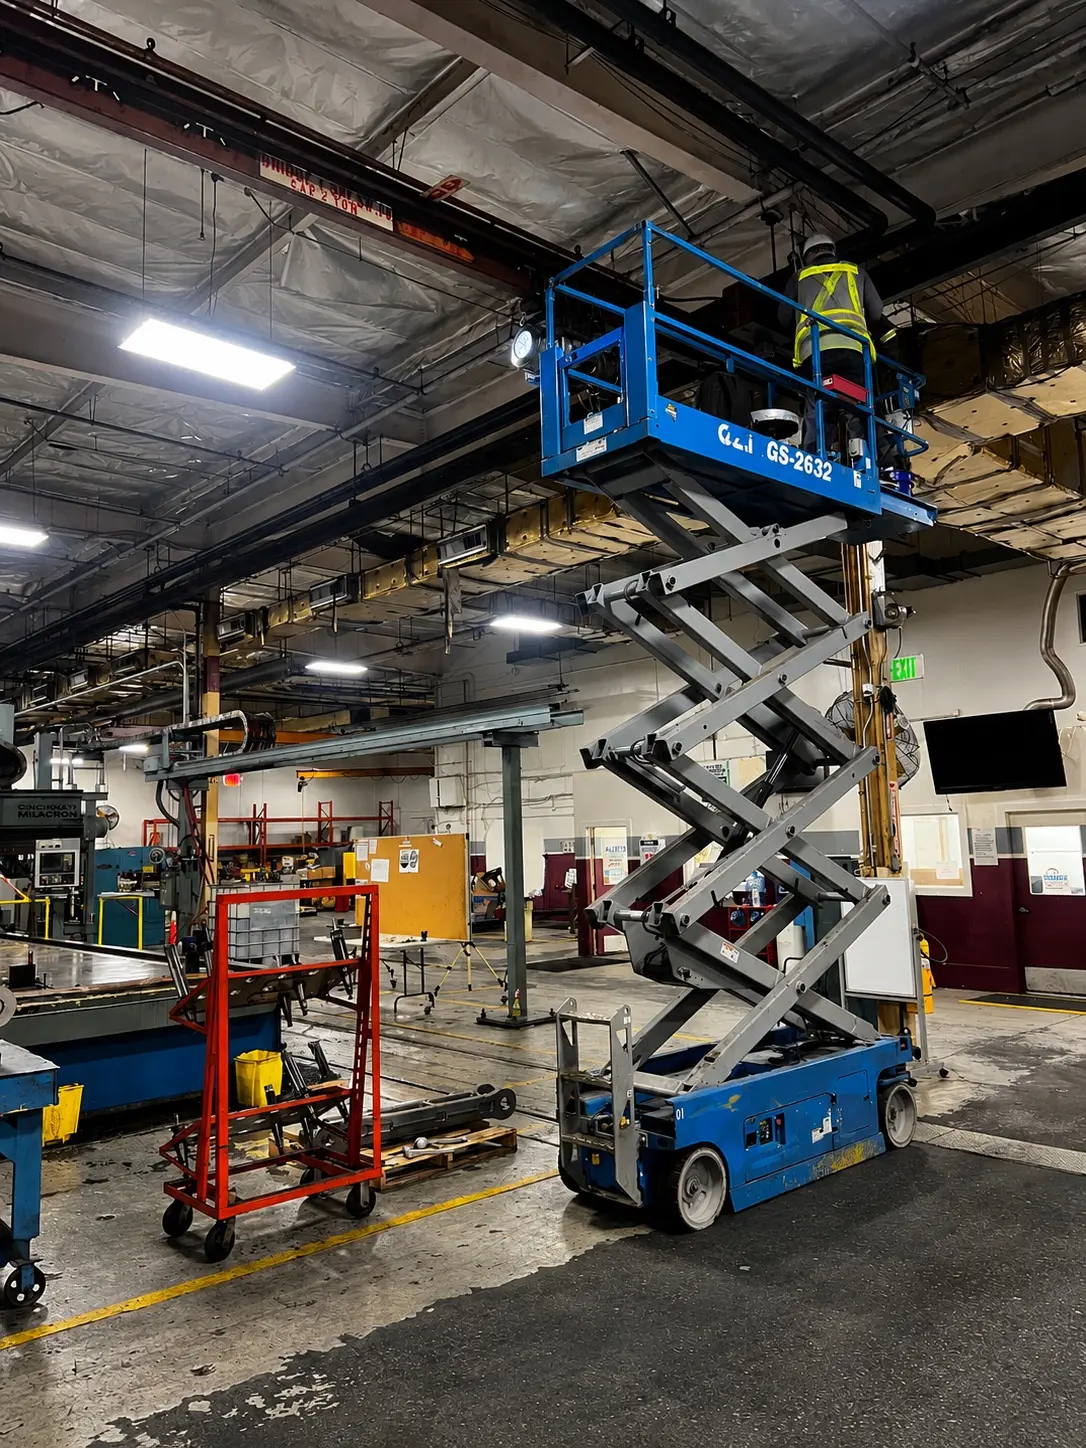 Fieldwork inMission Viejo
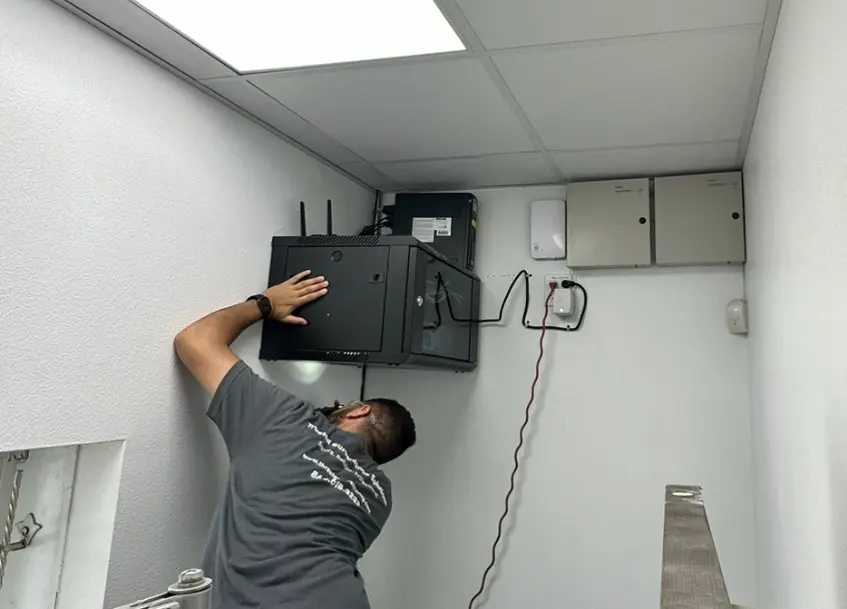 Fieldwork inCommerce
Where the system matters
Priority coverage and control areas.
Final placement is determined during a site assessment. These are the operational areas we would typically evaluate first for this type of property.
production transitions
labs and material storage
shipping
Complete Three Factor offering
Recommended security layers for pharmaceutical & medical-device manufacturing.
Every project is customized, but each assessment considers all 12 service categories so gaps are not left between systems.
01
Video security & intelligence
Security Camera Systems
Place high-resolution, low-light, panoramic, license-plate, or specialty cameras where appropriate around controlled entrances, production transitions, labs and material storage, and shipping. Recording, retention, analytics, remote viewing, and user permissions are designed together so footage is useful when an event occurs.
Service details02
Live oversight & remote visibility
Live Monitoring & Remote Site Surveillance
Combine trained operator monitoring with dependable remote visibility across controlled entrances, production transitions, labs and material storage, and shipping, especially during after-hours periods or where staffing is limited. Alarm events, priority video, and dispatch instructions are set up with our monitoring partner around how the site actually runs.
Service details03
Live remote guarding, intervention & response
Virtual Security Guard & Incident Response
Extend a trained remote security presence and documented incident-response workflow across priority areas such as controlled entrances, production transitions, labs and material storage, and shipping. Through our UL-listed monitoring partner, operators can run scheduled patrols, review verified events, and issue authorized talk-downs, then notify your contacts or coordinate approved dispatch.
Service details04
Intrusion & alarm protection
Alarm Systems
Put door, motion, and glass-break sensors where you need to know right away. Alarm zones and alerts follow your opening, closing, and after-hours routine.
Service details05
Visitor communication & entry
Intercom Systems
Give visitors, deliveries, customers, residents, and staff a clear way to communicate at controlled entrances, production transitions, and other entry points. Video or audio stations can route calls to the right desk, tenant, mobile user, or operations team and coordinate entry release when appropriate.
Service details06
Credentials, doors & gates
Access Control Systems
Control who gets in, from employees and residents to vendors and vehicles, using phones, cards, or fobs. Schedules and permissions can be managed for one building or many.
Service details07
Intelligent early warning
Early Detection Systems
Use suitable AI analytics, thermal imaging, perimeter sensors, and intelligent detection around controlled entrances, production transitions, labs and material storage, and shipping to surface unusual activity or developing threats earlier. Alerts, lighting, speakers, and escalation rules are tuned to the property’s schedules and operating risks.
Service details08
Gates, fencing & controlled access
Gates, Fencing & Perimeter Security
Secure the physical boundaries and controlled approaches around controlled entrances, production transitions, labs and material storage, and shipping with appropriate fencing, pedestrian gates, vehicle and driveway gates, automated gate operators, anti-climb details, barriers, and protective hardware. Where appropriate, LPR cameras can recognize approved vehicles and trigger authorized gate entry, while access-control credentials and video or audio intercoms can authorize and release connected gates or doors. Traffic flow, safety devices, egress, daily operation, lighting, cameras, and detection are coordinated as one perimeter and entry plan.
Service details09
PA, talk-down & emergency messaging
Security Audio & Emergency Communication Systems
Coordinate PA speakers, zoned paging, live talk-down, prerecorded warnings, duress inputs, and event-triggered announcements around controlled entrances, production transitions, labs and material storage, and shipping. Speakers, permissions, and integrations are designed together so your team can warn and direct people clearly.
Service details10
System takeovers, retrofits & modernization
Security System Upgrades & Modernization
Evaluate existing cameras, recorders, alarms, access control, intercoms, wiring, network, storage, power, software, credentials, and documentation serving controlled entrances, production transitions, labs and material storage, and shipping. We keep the equipment that still works and replace failing parts in phases, so you are not paying to start over.
Service details11
Strategy, planning & documentation
Consulting & System Design
Evaluate controlled entrances, production transitions, labs and material storage, and shipping as one operating environment before equipment or construction decisions are made. Consulting and system design documents the current gaps, the recommended coverage, and a phased plan and budget for this property.
Service details12
Inspection, testing & lifecycle support
Preventive Maintenance & System Health
Scheduled inspection and testing keep cameras, alarms, and entry systems working. Each visit documents what we found and what to fix first, before coverage or evidence is lost.
Service detailsOperational benefits
What a properly designed system can improve.
Faster investigationSearchable, properly retained video helps teams understand incidents without piecing together incomplete views.Stronger accountabilityAccess records and camera evidence clarify movement through controlled entrances and production transitions.Better responseVerified alerts and defined escalation procedures help the right person act with better information.Less downtimeHealth checks, documentation, and planned upgrades keep the system useful long after installation.Room to growWiring and storage are sized so you can add cameras, doors, or locations later.
Begin with a professional assessment